Industries We Serve

Bulk material handling & control solutions—built around your process, your standards, and your uptime goals.

Phenix Equipment helps plant teams reduce downtime, protect product quality, and simplify vendor management with industry-specific systems—from metal detection and sanitary conveyance to inspection, packaging, and turnkey integration.

Find your industry.
Get the right solution faster.

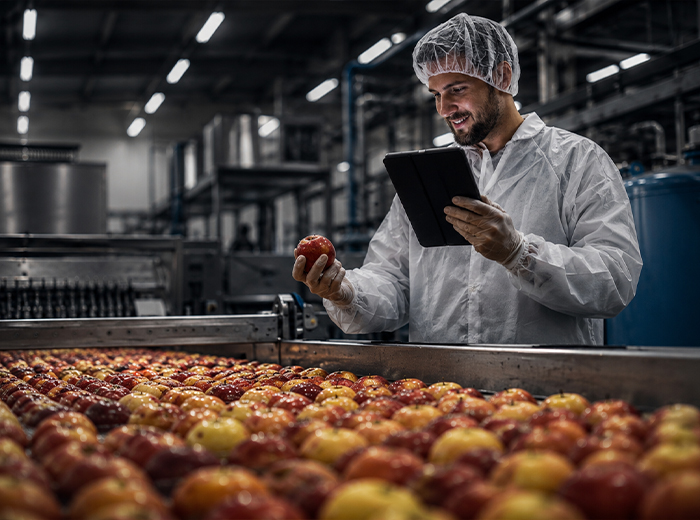
Food Processing

Reliable handling for critical powders and materials where consistency matters.

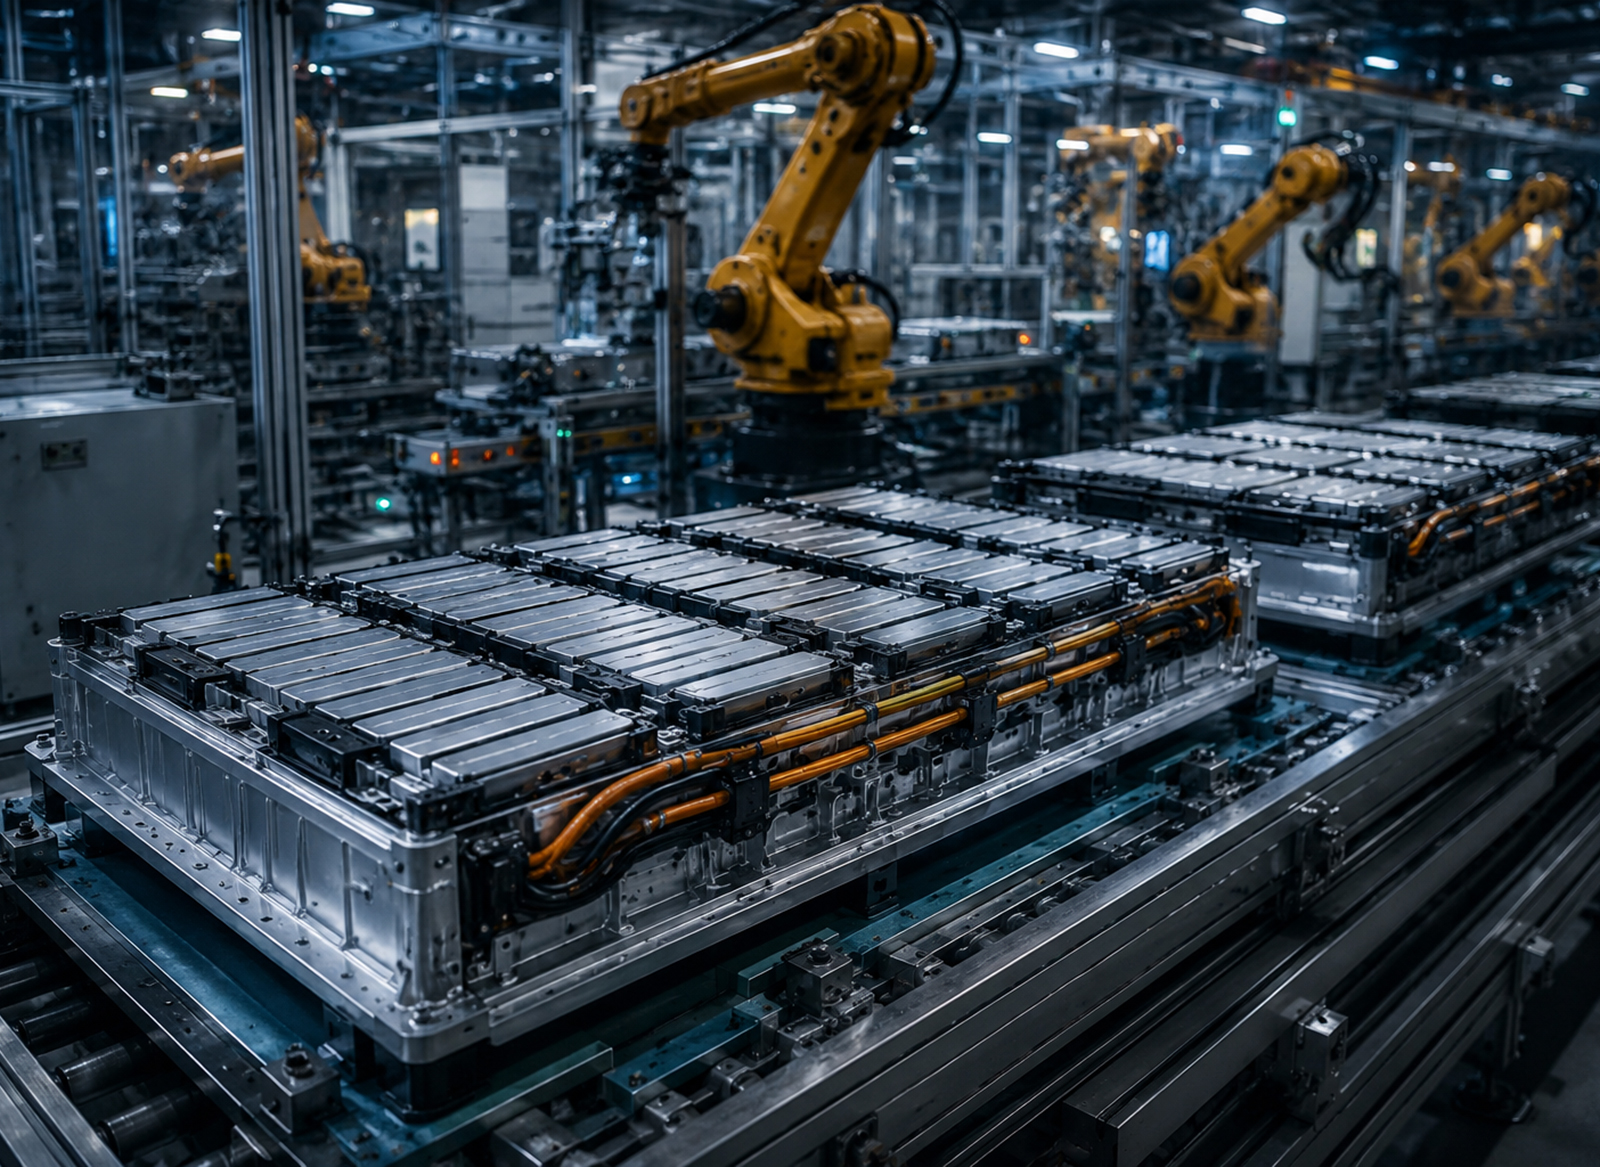
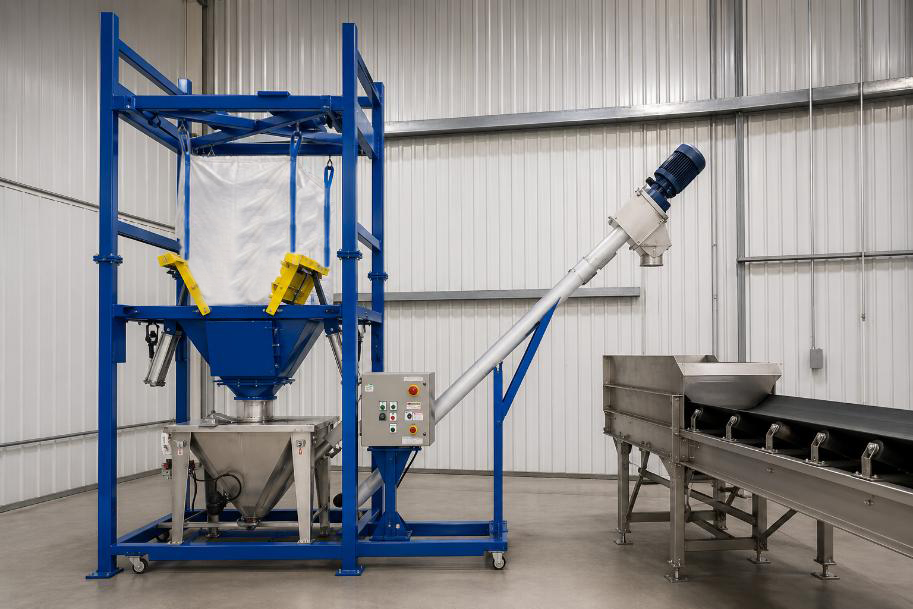
Batteries / EV Materials

Reliable handling for critical powders and materials where consistency matters.

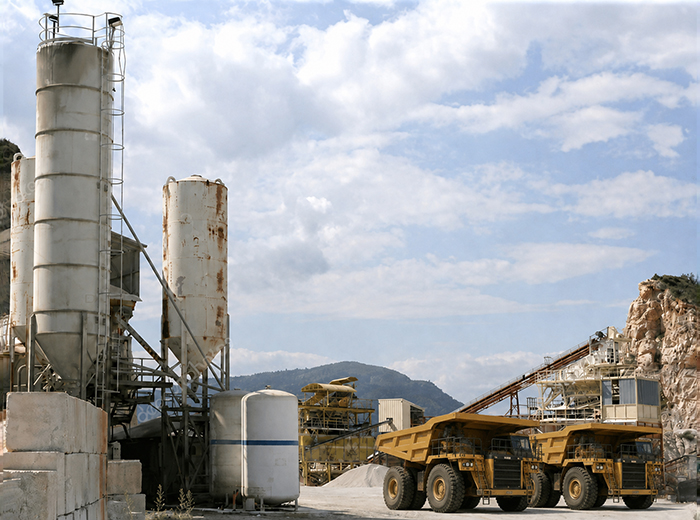
Aggregates & Mining

Reliable handling for critical powders and materials where consistency matters.

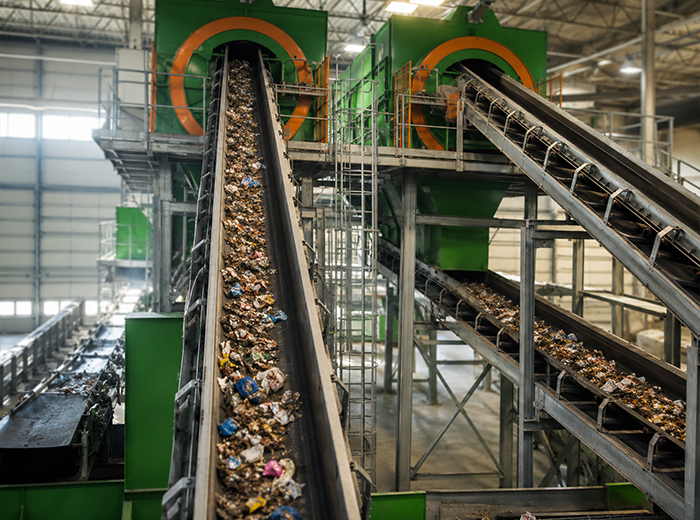
Recycling

Reliable handling for critical powders and materials where consistency matters.

Light Industrial

Reliable handling for critical powders and materials where consistency matters.

One partner. Fewer headaches. Better outcomes.

Single-source projects

Coordinate equipment, integration, and install support through one team

Designed for real plant conditions

Reliability, maintainability, and safety built into the system

Protect product & equipment

Metal removal, inspection, and control strategies that reduce risk

Built for growth

Scalable framework now, with a clear path to Quick-Ship/RFQ later

Food Processing

Sanitary, compliant systems that help protect product quality and reduce downtime.

Common needs we solve:

Typical outcomes:

Batteries / EV Materials

Material handling and control designed for high-spec environments—where consistency, containment, and process stability matter.

Common needs we solve:

Typical outcomes:

Aggregates & Mining

Heavy-duty systems built for harsh environments, high tonnage, and uptime-focused operations.

Common needs we solve:

Typical outcomes:

Recycling

Separation, sorting support, and metal removal that improves recovery rates and protects valuable equipment.

Common needs we solve:

Typical outcomes:

Light Industrial

A practical “catch-all” for manufacturers that need better flow, inspection, and handling—without overcomplicating the solution.

Common needs we solve:

Typical outcomes:

Built for plants in our region. Backed by proven manufacturers.

Phenix supports plant teams across Central & Northern California and Western Nevada with responsive expertise, practical solutions, and equipment partnerships that fit real-world demands.

Capability-driven recommendations (not just catalog links)

Support selecting equipment that fits your material and process

Local territory coverage with responsive follow-through

Ready to Improve Your System or Validate Your Magnet Program?

Tell us your industry, your goal, and your location—we’ll point you to the right next step.