Food Processing Equipment & Turnkey Solutions You Can Trust
Sanitary, compliant, and production-ready systems for metal removal, conveyance, inspection, and packaging—engineered for food processors across Central & Northern California and Western Nevada.
Food processors face a unique set of challenges: strict safety standards, contamination risk, washdown requirements, uptime demands, and constant pressure to simplify vendors.
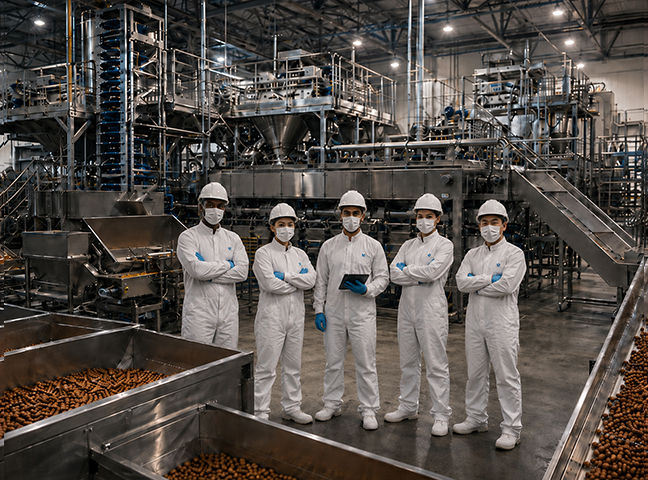
Phenix Equipment helps food processing facilities protect product integrity, maintain compliance, and keep lines moving with integrated solutions for metal detection, sanitary conveyance, inspection, and packaging. From single components to fully coordinated systems, we act as a single-source partner—reducing complexity while improving outcomes.
Key Problems We Solve
Common Food Processing Challenges
Risk of metal contamination and costly recalls
Sanitary design requirements (USDA, FDA, FSMA)
Frequent washdowns and harsh environments
Downtime caused by mismatched equipment vendors
Limited internal resources to manage multi-vendor projects
Our role:
Simplify procurement, integration, and support—without compromising food safety or performance.
Core Solution Areas
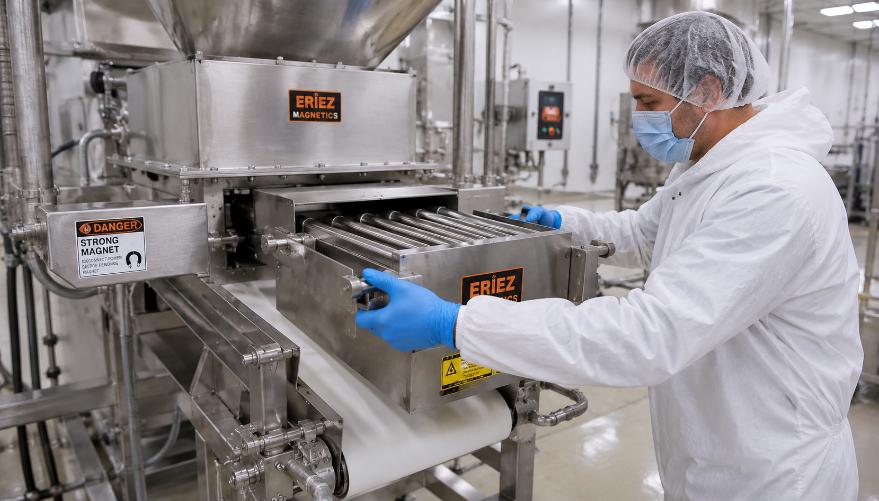
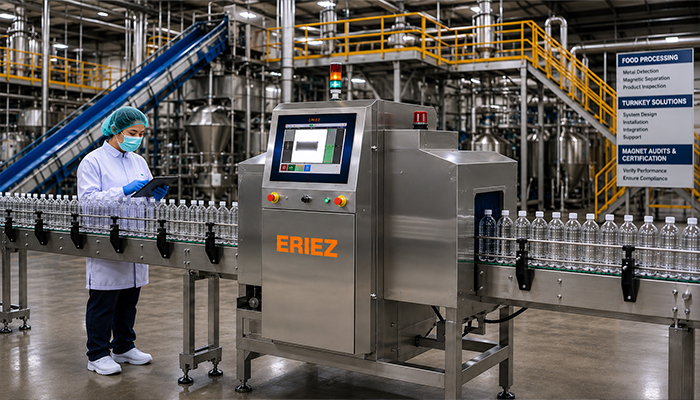
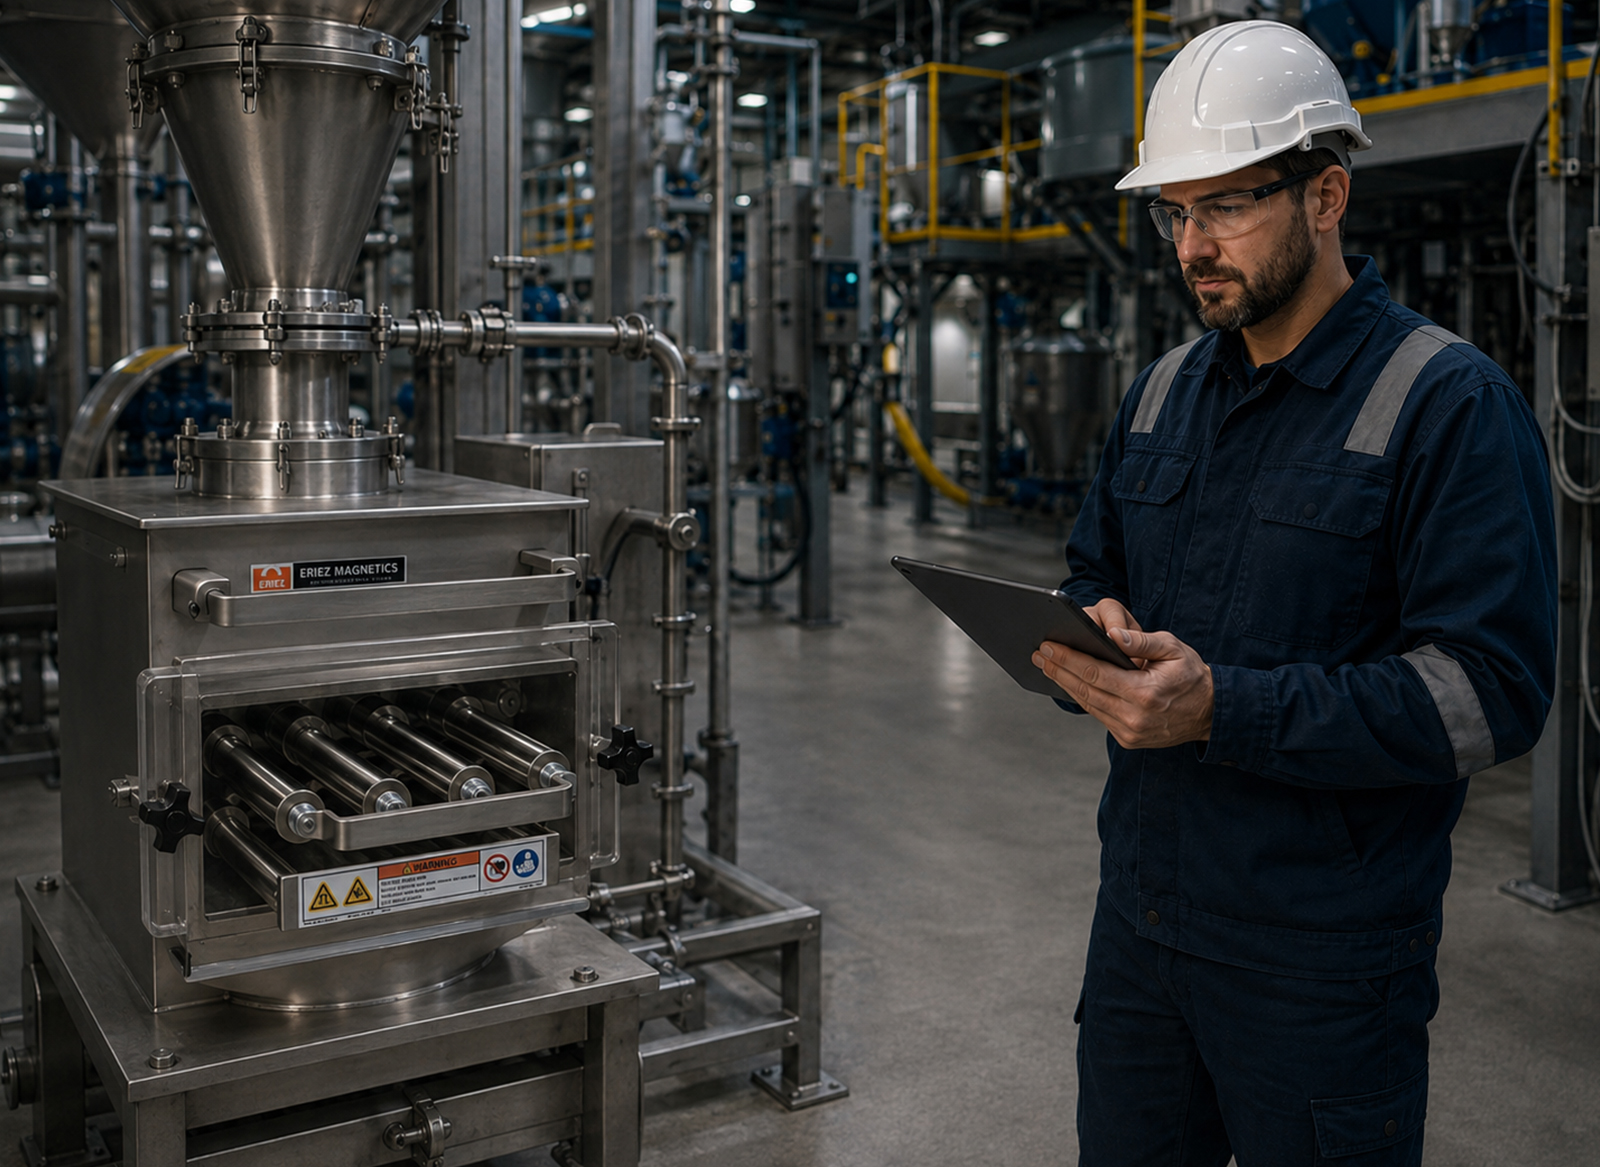
Metal Detection & Metal Removal
Protect your brand and your customers with proven metal control solutions.
Capabilities include:
Magnetic separators (grate, plate, drawer, drum, and inline magnets)
Metal detectors for raw and packaged products
Custom configurations based on product flow and risk points
Differentiator:
Magnet Audits & Certification to verify effectiveness and compliance