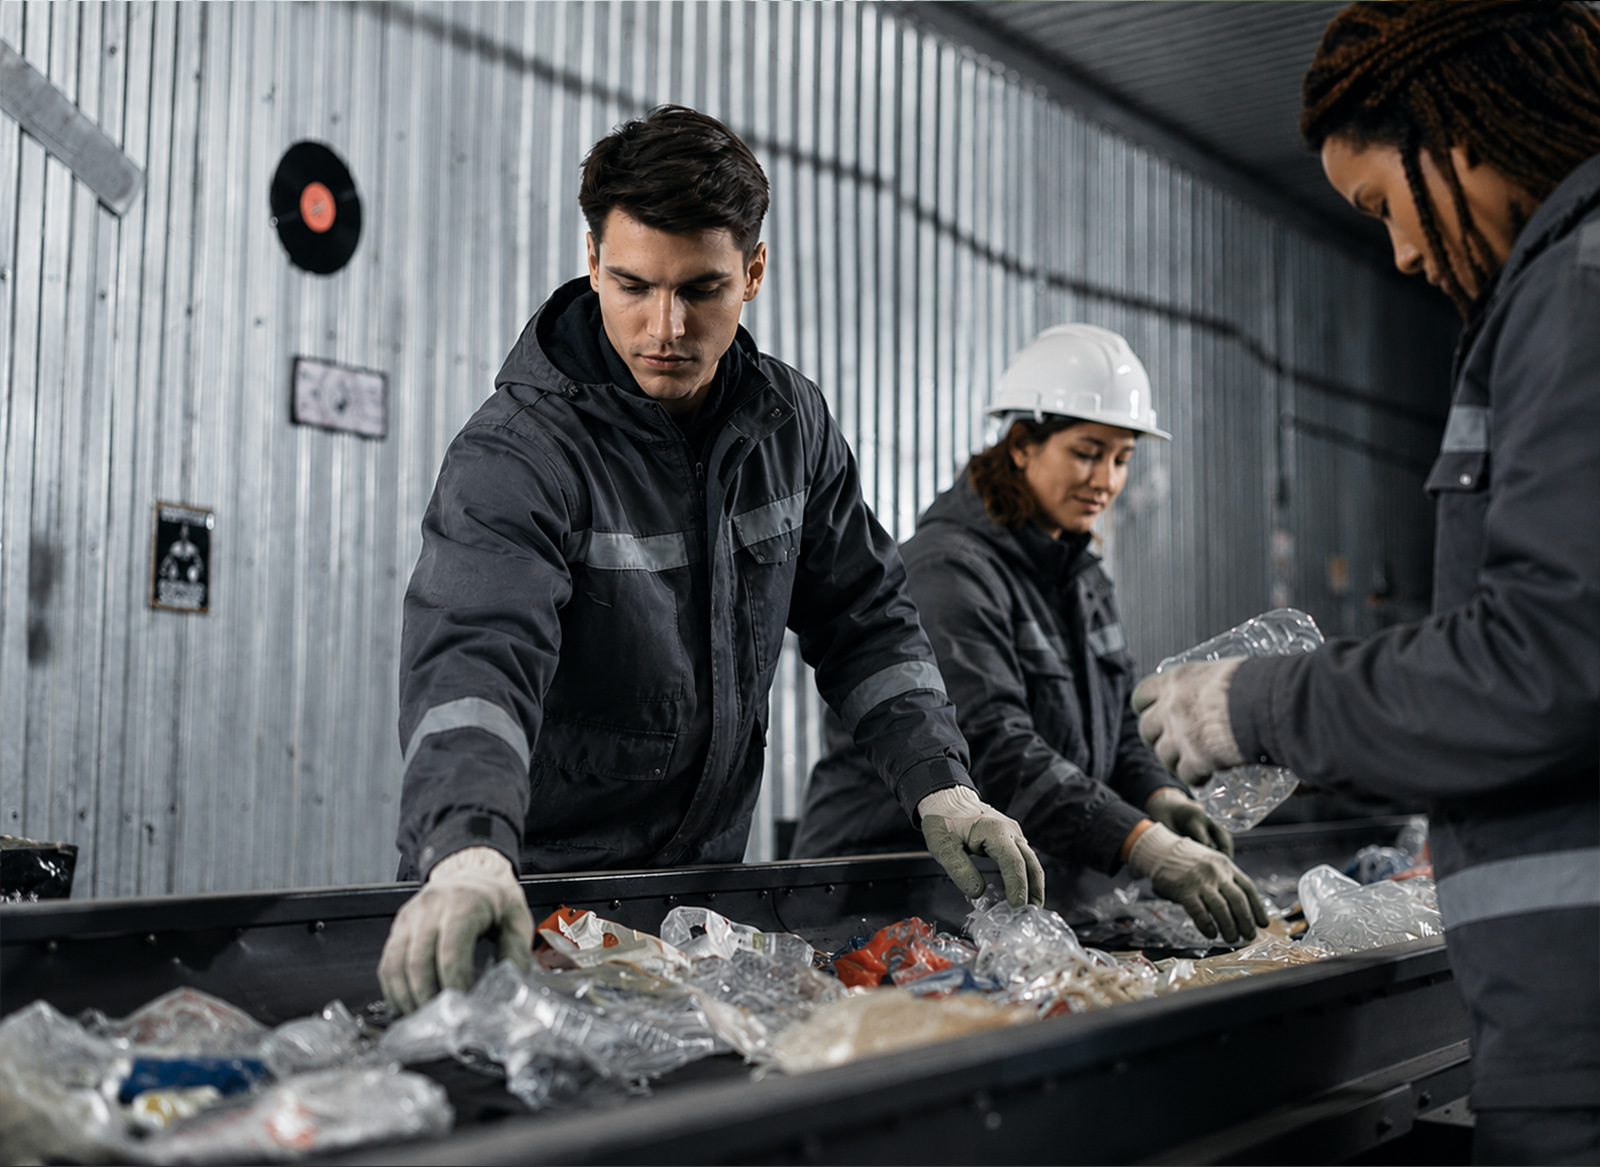
Recycling Smarter Material Recovery. Cleaner Outputs. More Profitable Operations.

Recycling facilities face constant pressure to improve recovery rates, reduce contamination, and keep operations running efficiently. From mixed material streams to abrasive environments, success depends on reliable equipment, proper separation, and systems that work together seamlessly.

Phenix Equipment partners with recycling operations across Central & Northern California and Western Nevada to deliver turnkey bulk material handling and separation solutions—helping you recover more value from every ton processed.
Challenges We Solve

Recycling environments are complex and demanding. We help address the most common operational pain points:

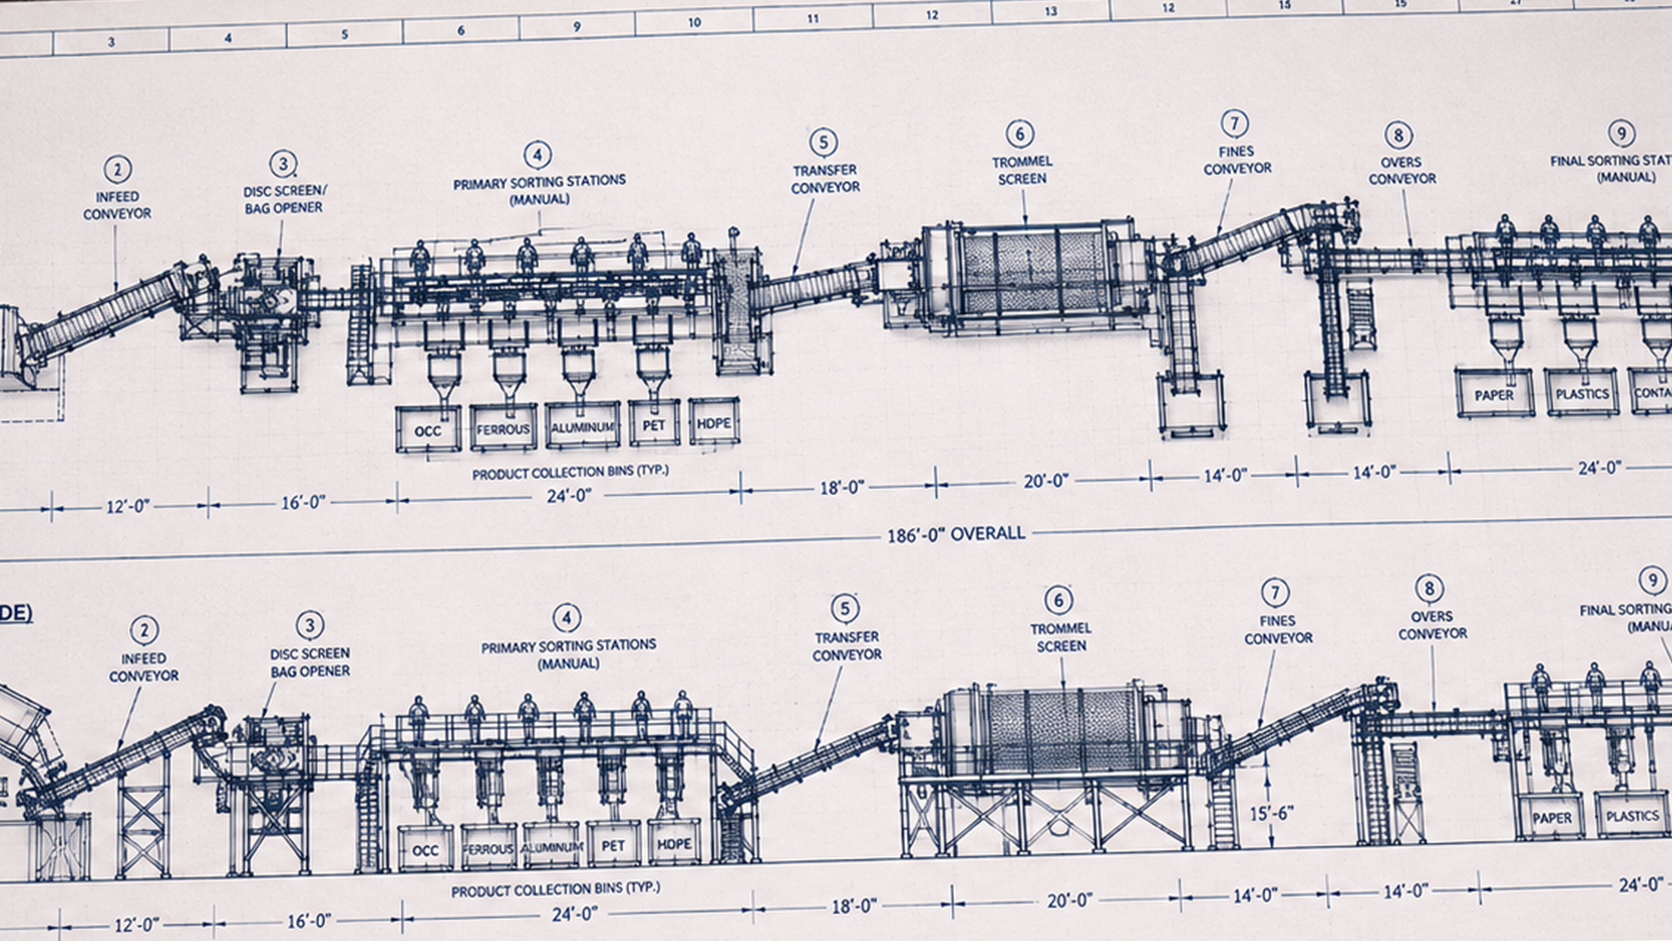
Turnkey Solutions for Recycling Facilities

We deliver single-source solutions that simplify your process and improve performance:

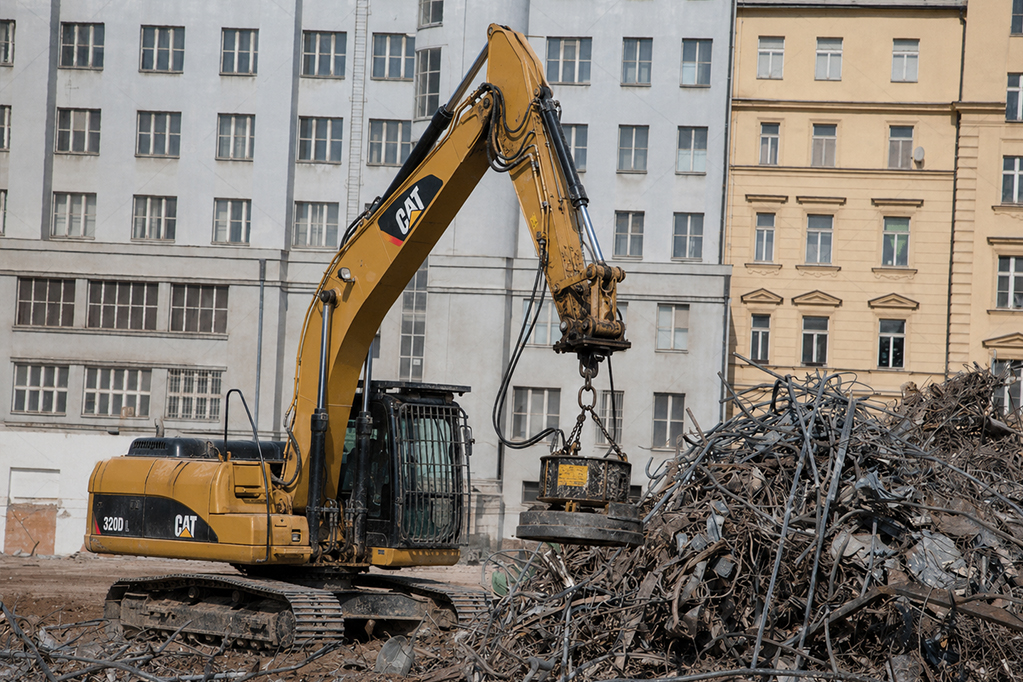
Magnetic Separation & Metal Recovery

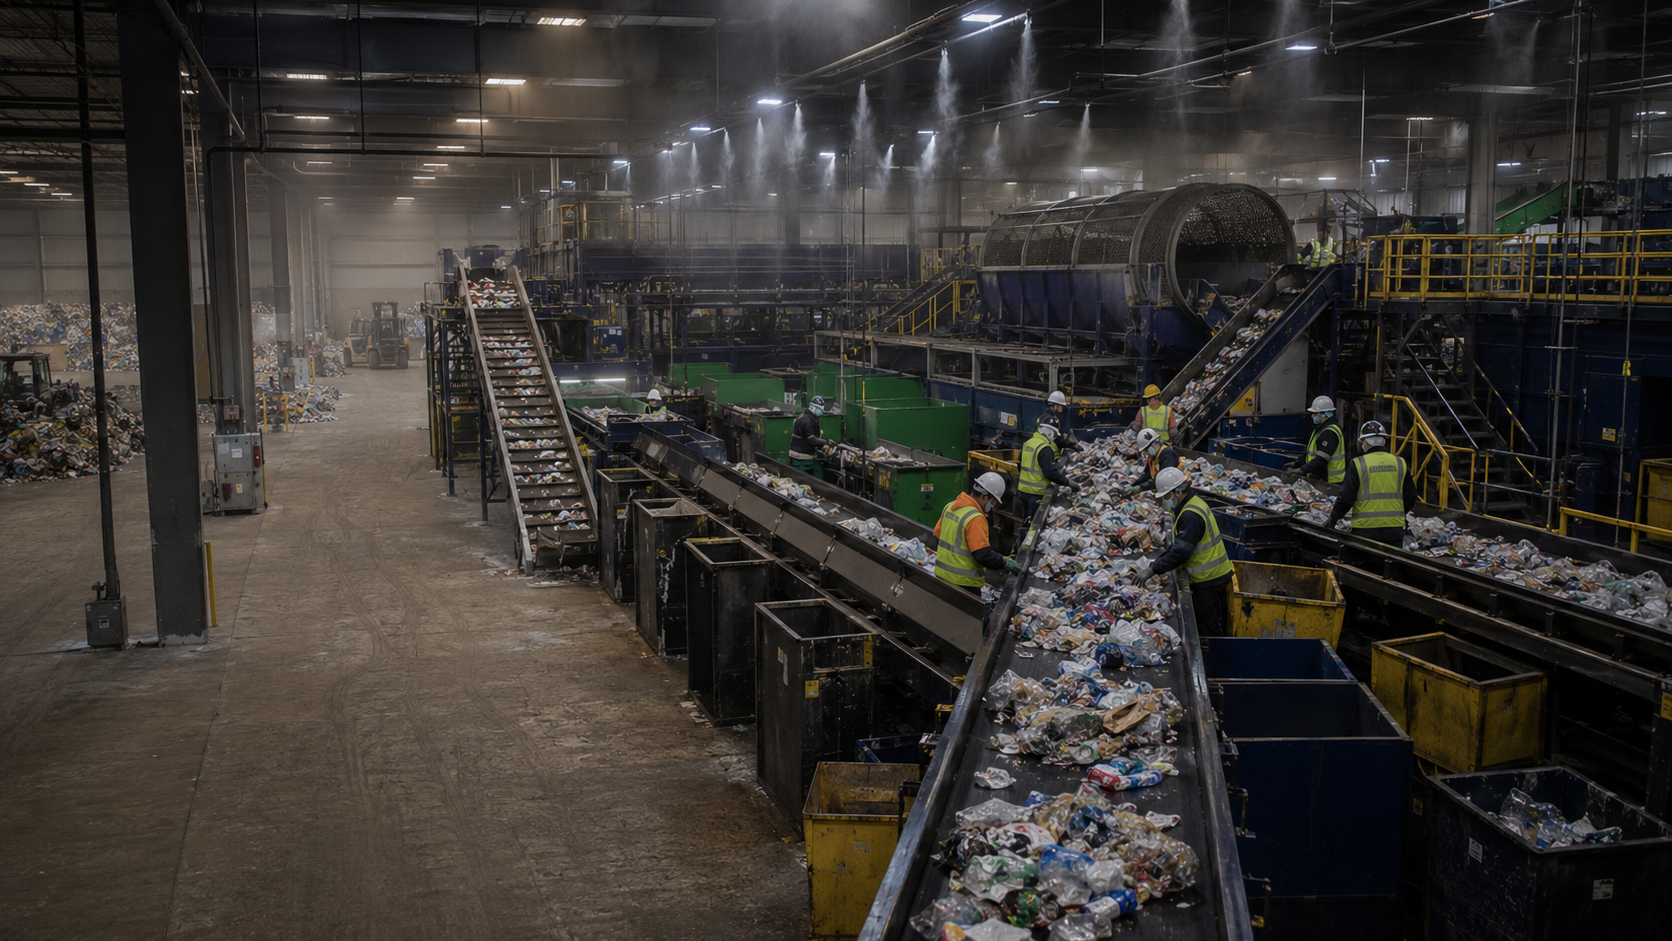
Conveying & Material Handling

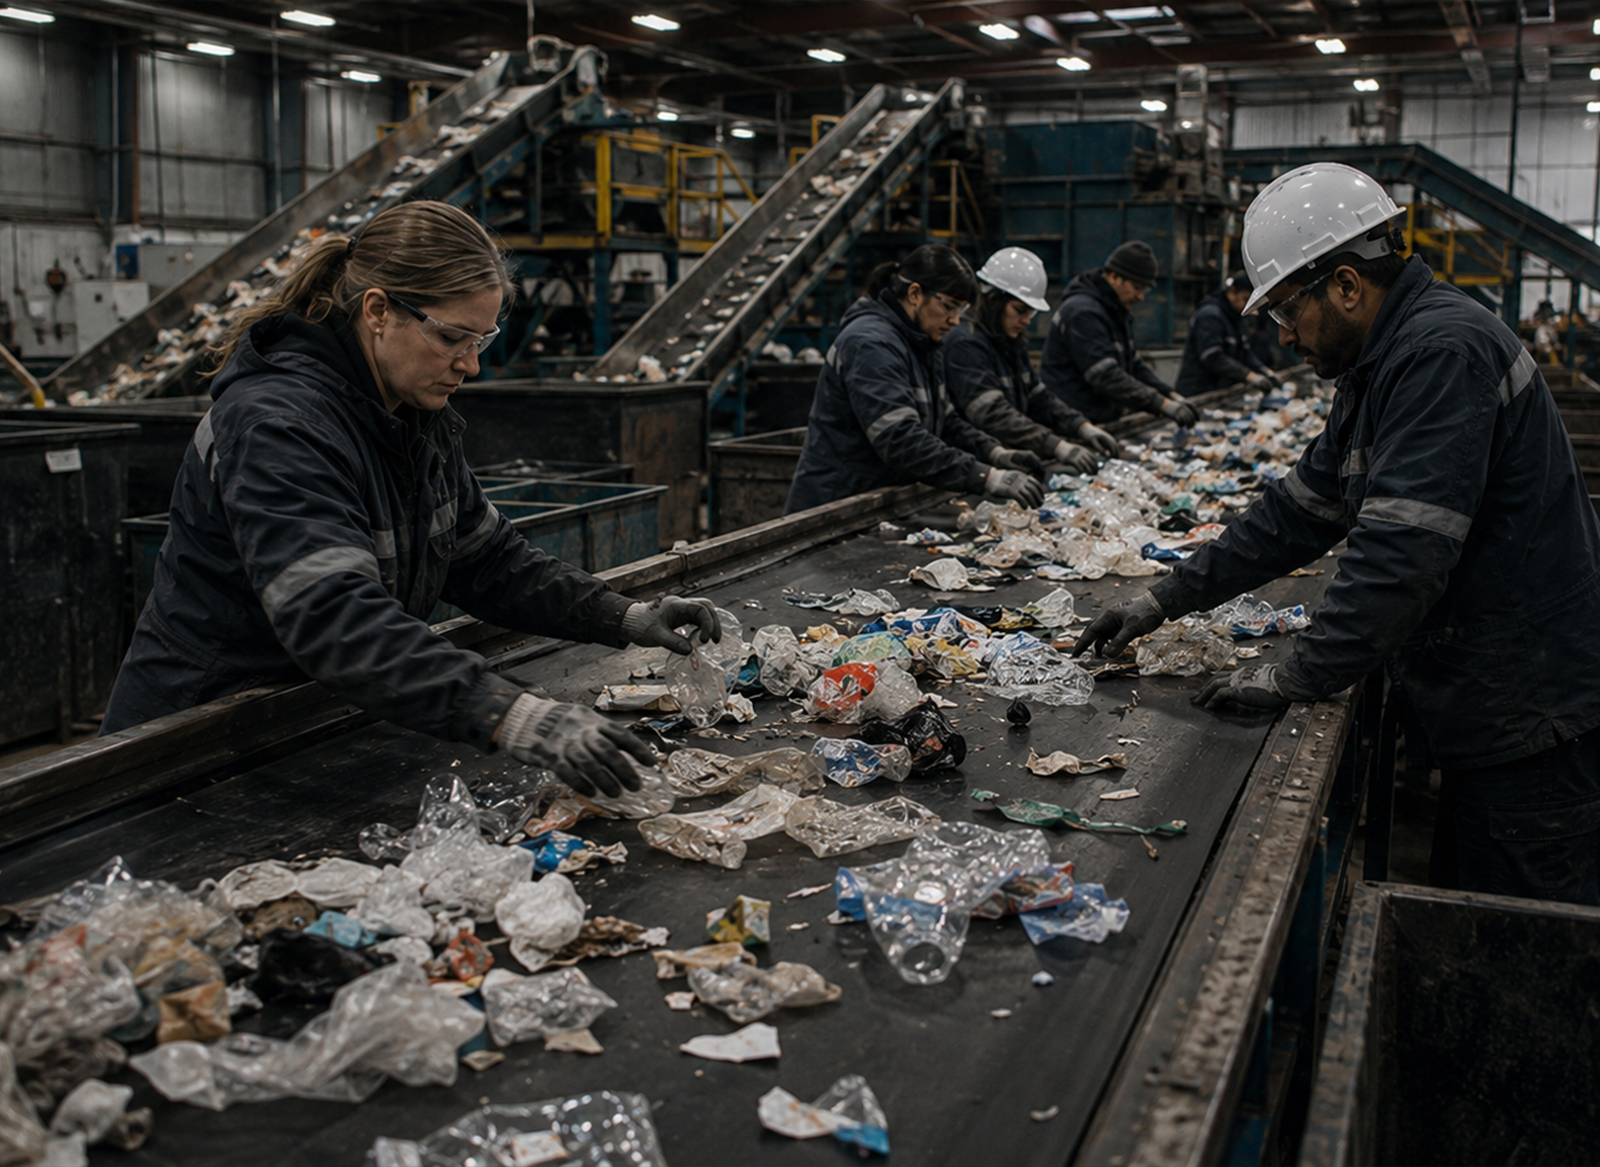
Screening & Sorting Support

Built for Demanding Environments

Recycling operations require equipment that can withstand constant impact, abrasion, and variability. We work with proven manufacturers to deliver solutions designed for:

Your Single-Source Partner

Managing multiple vendors can slow down projects and create unnecessary complexity. Phenix Equipment simplifies the process by acting as your single-source partner:

Let’s Improve Your Recovery Rates

If you’re looking to increase efficiency, reduce contamination, or upgrade your recycling systems, we’re here to help.
Talk to our team today to discuss your operation and identify the right solution.